The bore is part of the material decision
Define the supplied bar or blank separately from the finished joint. Mating fits, wear surfaces and later treatment belong on the drawing.
Select an image to open the full-size original and inspect its labels.
Key takeaways
- Select pin, bushing and coupling stock for their different working interfaces.
- For a mining pivot, review the pin, replaceable bushing and supporting lug bores together.
- Specify core properties and surface requirements separately, at the relevant section.
- Make the supplied stage explicit: bar stock, prepared blank or a separately agreed component scope.
Three components, three different jobs
Steel bar selection for pins, bushings and couplings starts with the drawing and the load path. A pivot pin can combine bending, shear and contact loading. A bushing has an inside wear surface and an outside fit. A coupling has to transmit torque while maintaining the required alignment and engagement.
| Component | Working interface | Put in the enquiry |
|---|---|---|
| Pin | Loaded section, bearing surfaces, shoulders and lubrication features | Core properties, local surface treatment, hardened depth where specified, finish and final fits |
| Bushing | Sliding bore, outer fit, wall and end faces | Mating pin, lubrication, wall after machining, treatment sequence and bore/OD tolerances |
| Coupling | Bore, keyway, spline, thread, flange or other torque-transfer feature | Torque and load cycle, engagement, alignment, notches, joining and inspection zones |
Include the mating material and lubrication arrangement. In a plain-bearing joint, both surfaces and the lubricant influence the outcome. Some bushing designs use bronze, composite or other bearing materials; a steel alternative needs the component designer’s approval.
Mining example: the bucket-to-stick pivot
Consider the bucket-to-stick pivot on an excavator working in mine maintenance or material handling. The bucket rotates about the pin; the pin and bushing contact surfaces see repeated movement, while the supporting lugs carry the joint into the machine structure. Abrasive contamination, lost lubrication and clearance growth all belong in the condition report.
Locate the joint before discussing its steel
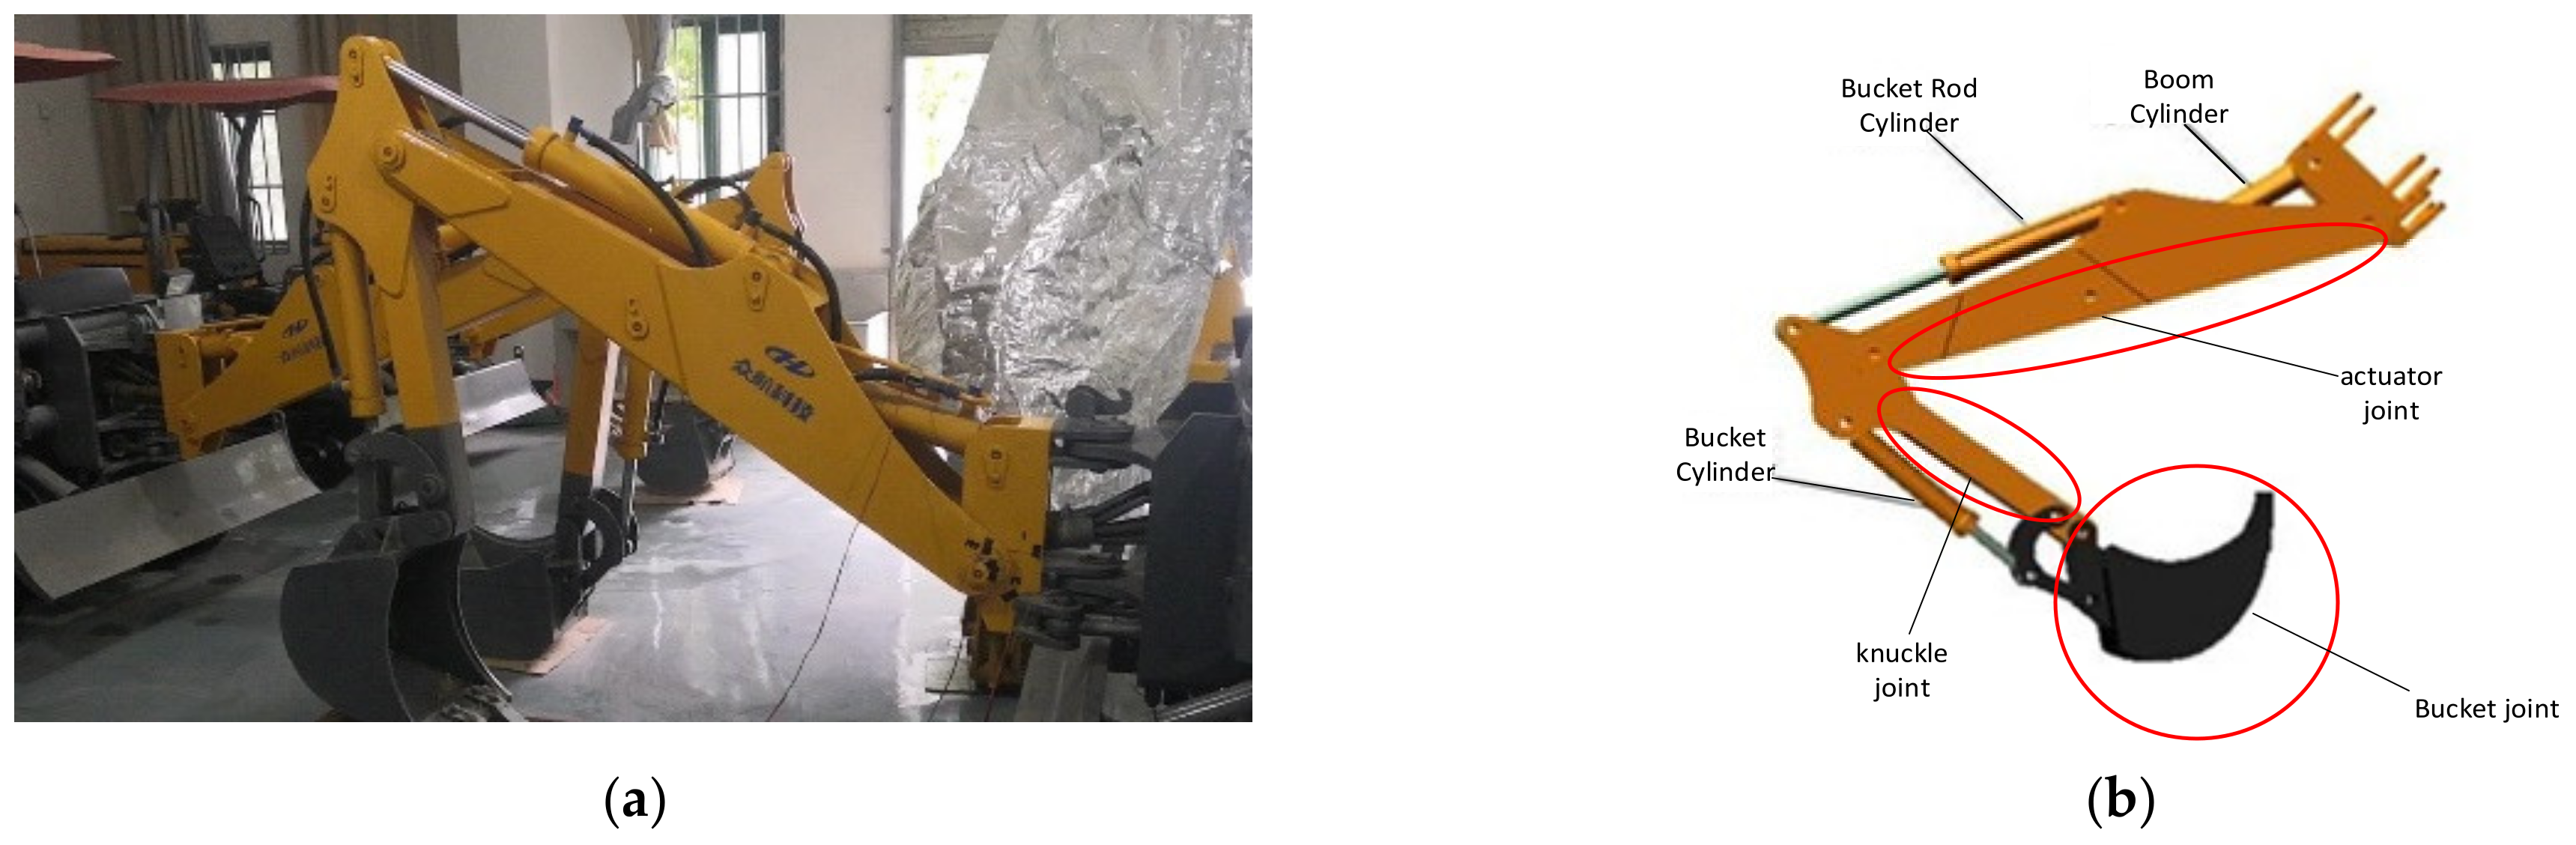
The study concerns a small utility excavator. The joint layout is useful context here; a mine’s larger machine needs its own drawing, loads and inspection limits.
Select an image to open the full-size original and inspect its labels.
Separate the pin, sleeve end and supporting plate
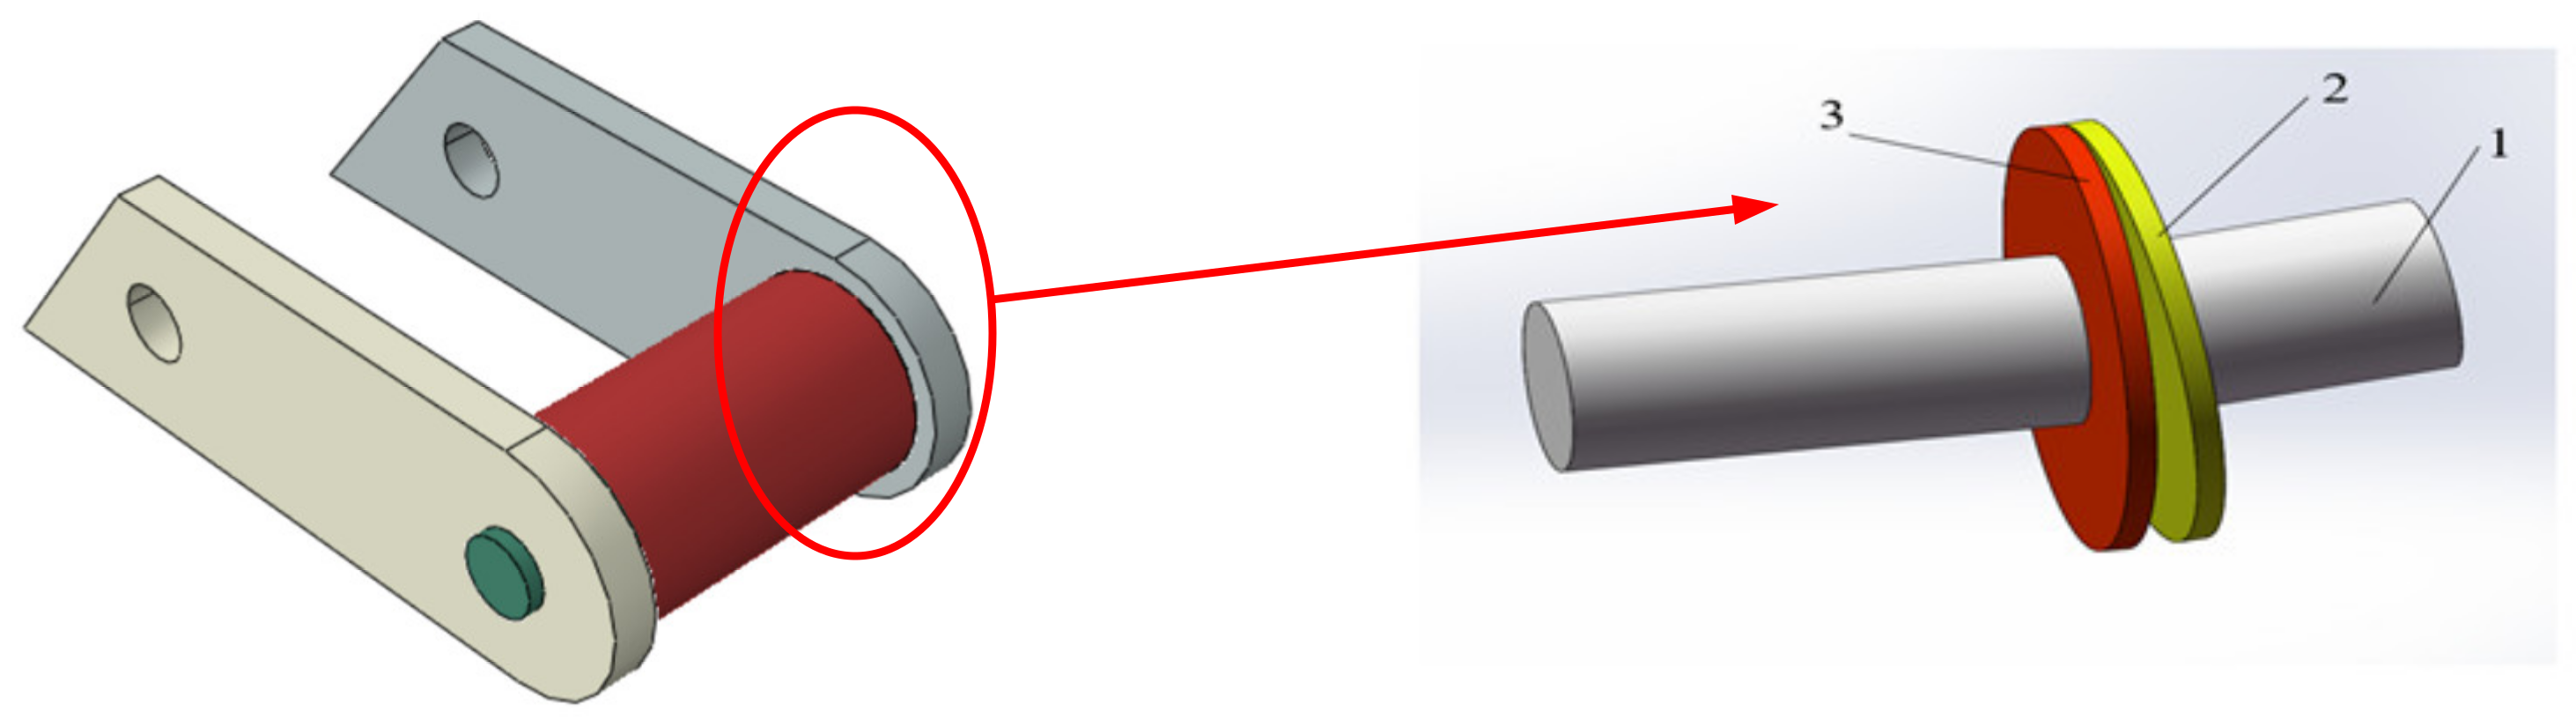
A worn end face is a different contact from the cylindrical sliding surface. Record the exact interface that is losing material.
Select an image to open the full-size original and inspect its labels.
Chen and colleagues combined a dynamic model, strain measurements and wear examination to investigate excavator joints, with particular attention to the bucket-joint end faces. Their work is a useful reason to inspect the sides of the joint as well as the pin diameter. [1]
| Location | Question for the workshop |
|---|---|
| Pin bearing surface | Is wear uniform, localised, scored or associated with poor lubrication? Record diameter and position. |
| Bushing bore and outside fit | Where is movement intended, and has the bushing moved in its housing? Measure both interfaces. |
| Lug/support bores | Are the bores aligned and within the approved shape and fit limits? Check for ovality and local damage. |
| End faces, seals and grease path | Is there side contact, contamination entry or a blocked lubrication route? |
| Pin shoulders and features | Where do grooves, steps, holes or retention features meet the highly loaded section? |
A published test: when one support takes more of the load
Karlsen, Lemu and Berkani compared five pin-joint arrangements, including cylindrical and expanding pins with different support-bore conditions. Their test pins had a nominal diameter of 88 mm; the circular support bores were 88.9 mm. Loads increased from 0 to 500 kN in 100 kN steps, with three loading repetitions at each step. [2]
The actual joint test rig
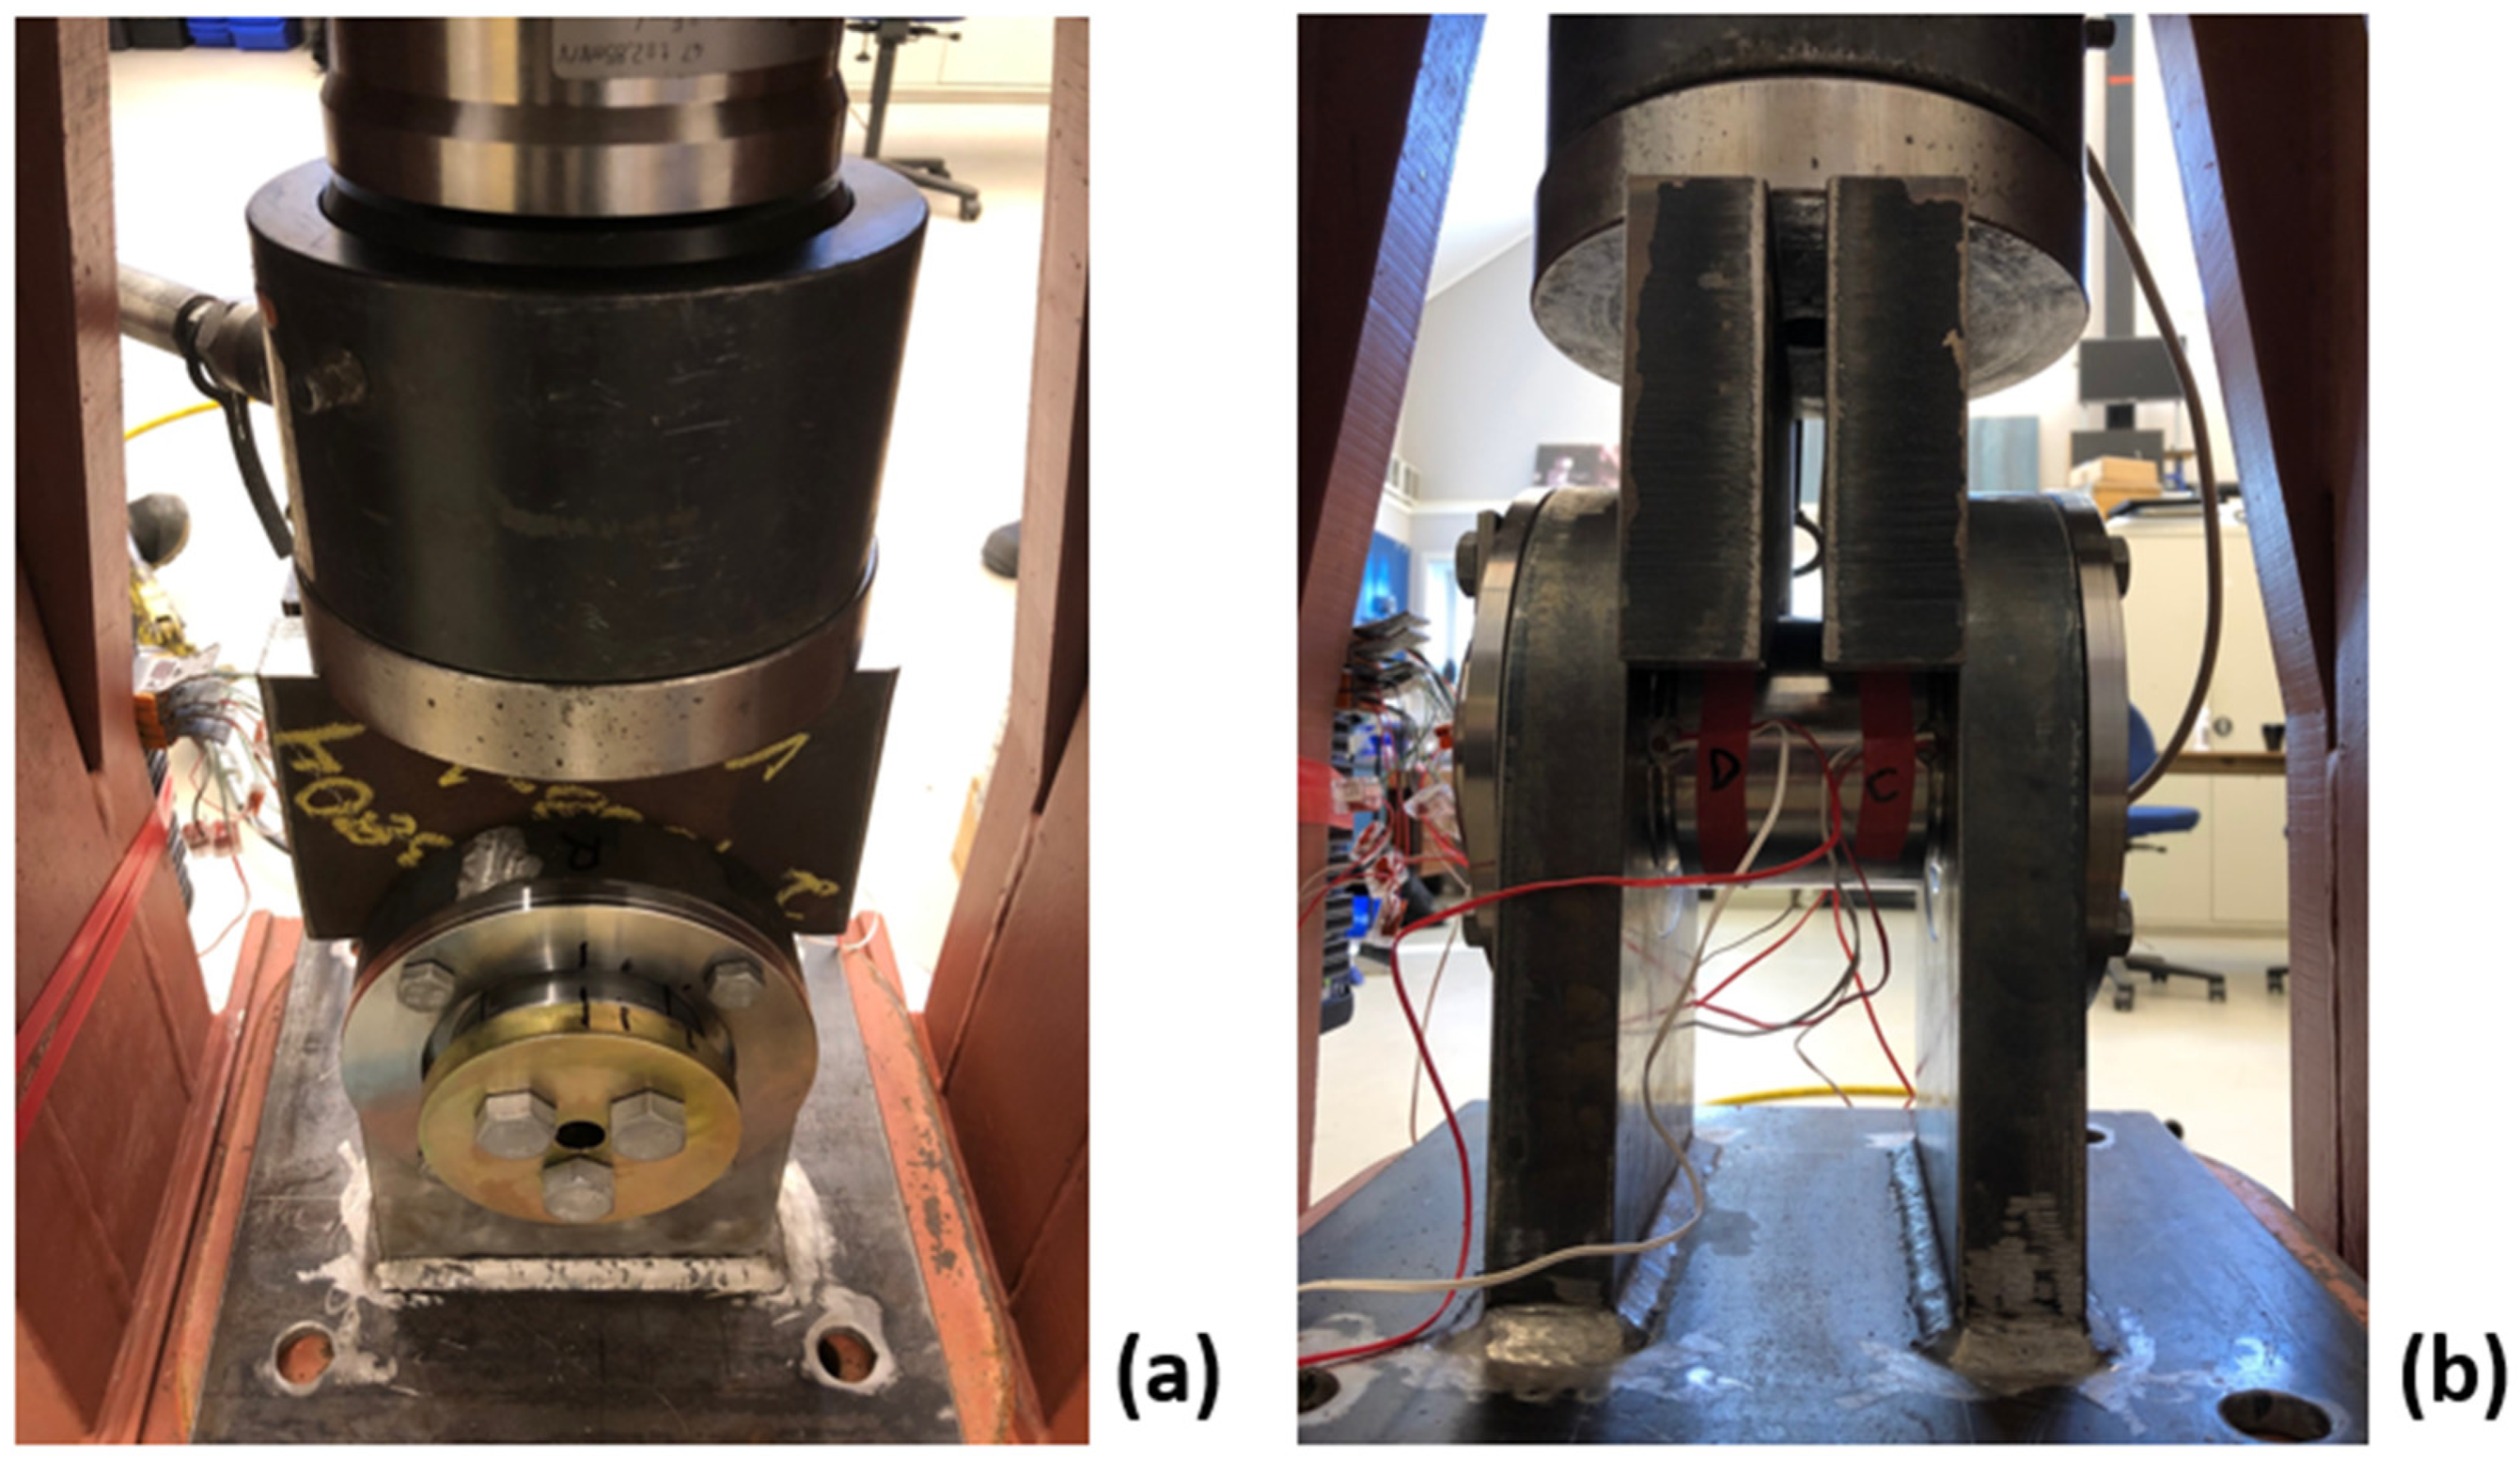
The researchers changed the support condition and measured strain near the pin ends. These are laboratory assemblies, not JOTAIN product qualification tests.
Select an image to open the full-size original and inspect its labels.
| Test | Pin / support arrangement | Installed diametral clearance |
|---|---|---|
| 1 | 88 mm cylindrical pin; circular supports | 0.9 mm at each support |
| 2 | Cylindrical pin; additional simulated wear at the left support | 0.9–5.9 mm left; 0.9 mm right |
| 3 | Expanding pin; circular supports | Zero after expansion at both supports |
| 4 | Expanding pin; additional simulated wear at the left support | 0–5 mm left; zero right |
| 5 | Expanding pin; damaged side repaired with the research insert | Zero after fitting at both supports |
In test 4, the authors reported that the right support took approximately five times the shear force of the left at maximum load. One end was fixed while the other remained partly loose. The load-bearing pins were EN 1.4418 stainless steel and the supports were S355; this was a support-condition experiment, not a comparison of 1045 and 4140. [2]
For the buyer, the point is straightforward: inspect the support before deciding that a stronger replacement pin will solve the problem. The experimental clearances and loads are not service limits for another machine. Repair geometry, material changes and return to service stay with the responsible equipment engineer.
Choose the grade at the section that will be treated
Separate the purchased bar diameter, the heat-treated section and the finished part. They may be three different dimensions. A large solid pin and a bored bushing of the same outside diameter also respond differently to machining and treatment.
A medium-carbon route such as 1045 and a chromium-molybdenum route such as 4140 should be compared against the required core properties, section and processing sequence. Do not turn the grade name into a fixed hardness or a service-life promise. State the property requirement and where it must be demonstrated.
ISO 683-1 and ISO 683-2 cover specified product forms and conditions for non-alloy and alloy heat-treatable steels. Their mechanical-property requirements have size boundaries. SAE J403 and J404 address the chemical compositions of SAE carbon and alloy steels. A cross-standard proposal therefore needs more than a similar grade label. [3] [4] [5] [6]
| Requirement | State explicitly |
|---|---|
| Material designation | Grade, product standard, edition and any permitted alternative |
| Core properties | Required strength/toughness, relevant section, specimen location and condition |
| Wear surface | Treatment method, hardness, depth definition and final grinding allowance where specified |
| Machining sequence | Before/after treatment dimensions, stock removal, datum control and finishing |
| Inspection | Actual results, traceability, dimensions and specified NDT method/coverage/acceptance |
Review the separate product routes for CK45 / 1045 bar and 42CrMo4 / 4140 bar. Select the exact designation and standard for the order; the paired website names are not blanket interchangeability approvals.
Keep the wear surface and the core on separate lines
A pivot pin may need a hard working surface over a core selected for the mechanical duty. Specify the surface requirement, effective depth where applicable and final diameter after finishing. Keep these separate from the core property requirement.
For a bushing, include the wall left after boring and finishing, the outer fit and the sequence of heat treatment and final sizing. For a coupling, call out the keyway, spline, bore or thread that carries torque and the transitions that concentrate stress. The same round bar can become very different components.
The supplied stage changes the inspection plan

Keep rough stock, treated stock and final working surfaces distinct on the enquiry. This photograph illustrates machining stages, not a named mining installation.
Select an image to open the full-size original and inspect its labels.
Allow for the material removed after heat treatment. If a surface-treated zone is to be ground, the finishing allowance and the required remaining depth must be coordinated. Put responsibility for those operations on the route sheet rather than leaving it between the bar supplier and the machine shop.
Tell us where JOTAIN’s supply ends
Specify the stage you need from JOTAIN: steel bar, a cut or rough-machined blank, or a separately agreed component scope. Attach both the supplied envelope and the finished drawing so the quotation covers the intended stage.
| Enquiry stage | Define at handover |
|---|---|
| Bar stock | Grade and standard, size, condition, surface, straightness, material tests and heat identity |
| Prepared blank | All bar requirements plus cut length, stock allowance, rough features and traceability after cutting |
| Finished component scope, if separately agreed | Drawing revision, final fits, treated zones, surface finish, inspections and responsible final approver |
Name who performs later hardening, grinding, coating and final inspection. Carry heat identity through cutting and machining, and define how each test represents the delivered material. A complete machine assembly or an approved OEM replacement is a different scope from a steel-bar order.
A workshop-ready enquiry
For the mining pivot example, send the pin and bushing drawings together with the support-bore condition report. For a new part, send the design requirements. For a replacement, add photographs of the worn interfaces and the maintenance findings.
- Component, equipment location, drawing number/revision and quantity.
- Supplied bar or blank dimensions and finished dimensions, in mm.
- Grade, product standard/edition and delivered treatment condition.
- Core property requirements; wear-surface hardness/depth and final finish where specified.
- Mating materials, fits, lubrication and relevant operating conditions.
- Test locations, NDT requirements, heat traceability and document set.
- Downstream operations and the final acceptance responsibility.
That is enough to begin a precise material and processing discussion without guessing the load from a photograph or choosing a grade before the interfaces are understood.
Questions buyers ask
Should mining pivot pins use 1045 or 4140 steel?
Select the route from the required core properties, treated section, surface treatment, loading and drawing. Compare the exact product standards and inspection requirements. Neither grade name alone establishes suitability for a particular mining joint.
Will a harder pin solve an oval support bore?
It does not restore the bore geometry or the intended support and fit. Inspect the pin, bushing and support bores together, and have the responsible engineer define any repair and return-to-service requirements.
Should a bushing use the same steel as its pin?
Not automatically. The material pair, lubrication, contact motion, wear strategy and bushing wall/fit all matter. Some designs use non-steel bearing materials. Follow the approved component design for the pair.
What changes when selecting steel for a coupling rather than a pin?
The torque-transfer interface becomes central: keyway, spline, thread, flange or other engagement. Include torque cycles, alignment, critical transitions, joining and inspection zones, as well as the supplied section and treatment condition.
What should accompany an RFQ for mining pin or bushing stock?
Send the drawing revision, supplied and finished dimensions, material and treatment requirements, mating interfaces, inspection schedule, quantity and delivery destination. For a worn joint, add the bore measurements, photographs and maintenance findings.
RFQ checklist
- Drawing/revision, component function and exact installed location.
- Supplied section, finished section, machining allowance and quantity.
- Material standard/edition, delivered condition and later treatment.
- Core properties, working surfaces, mating fits and lubrication.
- Traceability, actual test results, inspection scope and final acceptance.
References
- Analysis of Dynamic Wear Characteristics of Joint Contact Friction Pair of Excavators Working Device
Chen, X. et al. Lubricants 12(4), 113 (2024). Read the publisher’s full paper (PDF).
- A Novel Technique for Temporarily Repair and Improvement of Damaged Pin Joint Support Bores
Karlsen, Ø.; Lemu, H. G.; Berkani, I. Applied Mechanics 3, 1206–1222 (2022). Read the publisher’s full paper (PDF).
- ISO 683-1:2016 Non-alloy steels for quenching and tempering
- ISO 683-2:2016 Alloy steels for quenching and tempering
- SAE J403_202402 Chemical Compositions of SAE Carbon Steels
- SAE J404_200901 Chemical Compositions of SAE Alloy Steels
Inquiry support
Working from a part drawing?
For this review, send the component drawing, the loads and service environment, the section during heat treatment, and the inspection and acceptance plan. For a quotation, also include the quantity and destination.