
Design values, product acceptance, and information checks
Before writing a value, decide what decision it controls. A design minimum may come from the component calculation; a product-standard range may qualify a delivered bar; an incoming check may protect machining; and an informational reading may support investigation without rejecting material. Label each requirement so a valid result answers the purchaser's intended acceptance question.
Start with the material identity and state: grade and product standard, edition, product form, ordered and ruling section, heat-treatment condition, surface route, and downstream processing. Hardness depends on composition, microstructure, section response, preparation, and test method. Tensile properties depend on the material covered, specimen, orientation, and test conditions. Neither should be copied from a generic grade sheet and applied to every diameter or delivery condition.
Use the property source hierarchy. The drawing or project material schedule sets component requirements; the product standard can set values for a named grade, condition, and section; the test-method standard explains how the result is obtained; the inspection plan defines sampling and release; and the accepted PO resolves conflicts and deviations. ISO 6506-1, ISO 6507-1, ISO 6508-1, and ISO 6892-1 are method standards. They don't select the acceptance range for the steel order.

Test method follows material, section, and purpose
Brinell testing uses an indentation large enough to average a wider local area than common microhardness work and is often useful for bulk steel-bar controls, subject to the method's specimen and thickness rules. Vickers can cover a broad force range and supports localized or traverse work when the procedure, force, spacing, surface, and measurement are properly defined. Rockwell provides a direct depth-based scale but requires the correct scale, indenter, force, surface, thickness, support, and spacing. Procurement does not need to restate each method clause; it does need to name the controlled method and the product-specific choices left to the order.
Do not write HB, HV, or HRC as decoration. A complete Brinell result includes the accepted HBW designation basis; a Vickers requirement needs the HV test-force basis and any dwell variation required by the procedure; a Rockwell requirement needs the scale, such as HRC only where appropriate. The test laboratory should apply the current controlled method, while the RFQ defines material state, location, target, sample extent, and reporting.
Tensile testing provides properties that hardness cannot directly replace: yield or proof strength, tensile strength, elongation, and often reduction of area when the product route requires it. ISO 6892-1 defines room-temperature tensile testing. ASTM A370 supplies test methods and definitions for mechanical testing of steel products in ASTM routes. Choose the method required by the controlling product specification; do not ask a supplier to certify simultaneously to both merely because both are familiar.
Use the matrix below to make quotations comparable. There is no generic steel hardness range or conversion table here. Acceptance values must come from the controlling grade/condition/section requirement or the purchaser's approved schedule.
| Requirement type / method | What the value means | RFQ fields that must be fixed | Common buyer error |
|---|---|---|---|
| Brinell hardness — ISO 6506-1:2014 | An indentation-based hardness result using the specified ball, force and measurement procedure; useful only for the tested state and location. | HBW designation/test basis, target, delivery state, surface preparation, indentation location, distance from ends, sample frequency, individual/average rule, and reporting. | Writing only 'HB 280' or treating a single end/surface reading as proof of uniform hardness through a full production section. |
| Vickers hardness — ISO 6507-1:2023 | An optical indentation result whose test force and preparation affect the represented scale and usable location, including traverse work when properly planned. | HV force basis, target, material state, preparation, traverse geometry or locations, impression spacing, frequency, acceptance, uncertainty/retest treatment, and report fields. | Comparing different HV forces or polished laboratory traverses with rough production-surface readings without an agreed method and representation. |
| Rockwell hardness — ISO 6508-1:2023 | A depth-based result on a named Rockwell scale using the scale-specific indenter and force sequence. | Exact scale, target, test surface and support, part/bar thickness suitability, location, spacing, number of readings, frequency, disposition, and reporting. | Writing a value without the scale, testing a curved or unsupported surface without an approved basis, or converting another scale informally for rejection. |
| Room-temperature tensile properties — ISO 6892-1:2019 | Properties determined from a tensile specimen, potentially including Rp0.2 or yield, Rm, elongation and reduction of area as required by the product/order basis. | Required properties and units, specimen geometry, orientation, radial/axial location, section covered/condition/lot, method options where relevant, frequency, acceptance, and retest. | Assuming a small coupon, near-surface specimen, or separately heat-treated test piece proves core properties or finished-component performance. |
| Steel-product mechanical testing — ASTM A370-26 when invoked by the ASTM product route | ASTM methods and definitions used with the applicable steel-product specification; A370 itself cannot choose the grade's acceptance values. | Applicable ASTM product specification and edition, specimen and location rules, ordered properties, condition, lot/frequency, permitted test route, rounding/retest, and certificate content. | Ordering 'to A370' as though it were a material grade or copying ISO values into an ASTM route without reconciling product and sampling clauses. |
| Inspection document — ISO 10474:2013 | A document type supplied according to the accepted order; its value comes from the actual ordered results and traceability it contains. | Document type, issuer/validation route, heat and lot identity, actual test results, methods, specimen locations, deviations, linked reports, review timing, and release approval. | Requesting an MTC or certificate type but never listing the tests, actual results, traceability depth, or pre-shipment review needed. |
Surface preparation, location, curvature, and section
A hardness reading is local. Scale, decarburization, grinding damage, surface roughness, curvature, insufficient thickness, poor support, nearby impressions, temperature, and preparation can bias or invalidate it. The test-method standard controls technical suitability, while the purchase specification should identify the acceptance surface and preparation. State whether scale is removed, how much stock may be removed, whether a curved-surface correction or approved fixture is needed, and whether the tested surface remains on the final product.
For bars, define axial and radial location. Routine production checks might be taken at an agreed end distance and surface preparation, while qualification may require a transverse slice with surface, mid-radius, and center points. If a hardness traverse controls case depth or through-hardening response, provide a sketch, origin, spacing, force/scale, edge exclusions, number of traverses, target curve or points, and treatment of a single outlier. Do not allow a supplier to choose the easiest location after seeing the result.
Tensile specimen representation needs the same discipline. Link specimen to heat, product, diameter, heat-treatment lot, bar or prolongation, orientation, and radial/axial location. State whether it is full-size or machined and which standard/product clause controls. If a large production section is critical, engineering should specify the required core or section evidence rather than inferring it from a surface hardness-to-tensile conversion.
For Rockwell testing, NIST specifically discusses specimen support and surface preparation as sources of measurement error. Review the fixture and prepared area when interpreting an unexpected HRC reading on a bar. Keep the method, location and product condition with that reading, and use the ordered test standard to decide whether it is valid. [8]
Lot, frequency, rounding, retest, and reporting
Sampling language should connect test frequency to the process that can vary. Define a lot using heat, diameter or section, delivery condition, and heat-treatment batch or continuous-furnace campaign as appropriate to the product route. 'One test per shipment' can conceal multiple heats and thermal lots. Testing every bar, however, may add cost without improving the decision when the property is qualified on a properly controlled batch. Ask quality and engineering to choose the lot unit before soliciting bids.
Write how results are judged. State whether every reading must fall within a range, whether an average is allowed, how results are rounded under the controlling method or product standard, and what happens after one nonconforming result. Retest, resampling, re-heat-treatment, sorting, concession, rejection, and reporting are different dispositions. Do not let a supplier invent the rule after testing. Any concession should identify affected heat/lot/bar identity and receive the required purchaser or customer approval.
ISO 10474 defines inspection-document types, but the PO must list content. Require actual values rather than 'pass' where the result matters: method and scale; specimen or indentation location; material condition; heat and lot identity; individual readings where required; averages only if authorized; tensile specimen data and results; equipment or laboratory evidence when specified; deviations and retests; and links to separate reports. Make bundle or piece marking reconcile with the certificate and packing list.
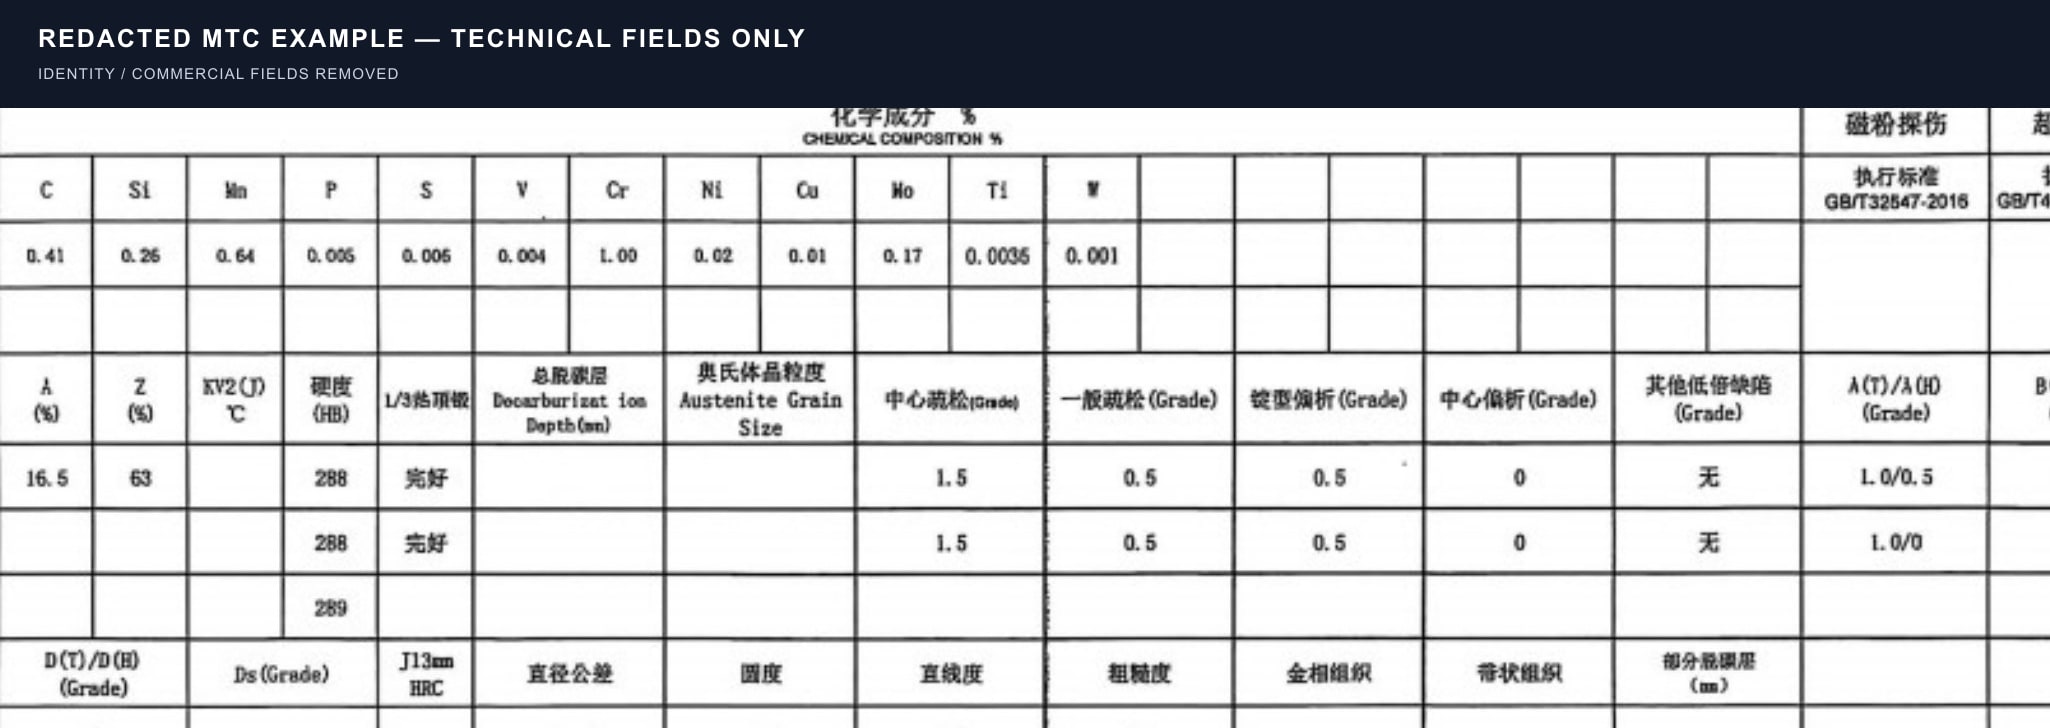
JOTAIN's redacted 42CrMoA MTC sample records 288, 288, and 289 in the HB column. Transcribe them as individual readings and preserve the HB label. Acceptance ranges come from the approved property schedule; a surface-to-core profile needs test locations. Request the full test designation, sampling locations, and lot identity in the complete report before comparing results with the ordered requirement.
Document pre-review isn't necessarily release. If the buyer needs a hold point, state the submission deadline, reviewer, allowed response time, closure of comments and nonconformances, and written shipment approver. For third-party inspection, define witness points and notice. These controls prevent a technically detailed certificate from arriving only after the material is already in transit.

A complete RFQ line
Use a single mandatory property schedule and ask suppliers to identify comply, deviation, or not applicable for every line. The quotation should state the exact test-method edition, proposed sample plan, material state, location, included reports, subcontracted testing, exclusions, and any price or lead-time effect. If a supplier proposes another hardness scale, sampling frequency, or certificate route, require the technical comparison and written purchaser approval before manufacture.
The sample below keeps targets in brackets because the correct values must come from the approved product standard, drawing, or project schedule. It is safer to leave a visible engineering input open during RFQ preparation than to paste a typical web value into a purchase order. Once approved, remove the brackets and lock the revision and deviation status.
At bid review, reject ambiguous phrases such as 'standard hardness,' 'high strength,' 'as per mill practice,' or 'MTC included' unless the offer maps them to the requested method, value, lot, sampling and evidence. Check that the certificate will identify the same heat, condition and section as the shipment.
Item: Heat-treated alloy-steel round bars for [component / drawing revision], Ø[diameter] × [length], [quantity]
Material: [grade] to [product/material standard and edition]; no unapproved equivalent designation or cross-standard property substitution
Delivery condition: [thermal condition] and [hot rolled / peeled / ground / machined surface]; ruling section [definition]; supplier to declare heat-treatment and straightening sequence
Hardness: [HBW / HV force / HR scale] [approved range], method [ISO 6506-1:2014 / ISO 6507-1:2023 / ISO 6508-1:2023], preparation [state], locations [sketch], [readings] per [heat-treatment lot], individual/average and retest rule [state]
Tensile: [Rp0.2, Rm, A, Z as applicable] to [ISO 6892-1:2019 or ASTM A370-26 only as required by the controlling product route]; specimen geometry, orientation, radial/axial location and section covered/lot per attached schedule
Sampling: Lot = [heat + diameter + condition + furnace batch]; [frequency]; no pooling of unlinked heats or thermal lots; nonconformance and retest disposition per [clause]
Inspection: Dimensions, straightness, surface and marking plus the ordered hardness/mechanical tests; third-party witness or hold points [state if required]
Certificate: ISO 10474 type [state type] with actual individual/approved average results, methods, specimen/indentation locations, heat, process-lot, bar/bundle traceability, retests, deviations and linked reports
Supplier response: State proposed methods, locations, frequency, included/subcontracted work, exclusions, price and lead-time effects, and every deviation
Packing / destination: [preservation, supports, bundle mass, port, Incoterm]Questions buyers ask
What should buyers send for hardness requirements?
Send the grade/product standard and edition, delivery state, section, approved target, complete method and scale/force, preparation, axial/radial locations, number of readings, lot frequency, individual/average rule, retest disposition, actual certificate fields, application, and drawing revision.
Should mechanical properties be listed in every steel bar RFQ?
No. List them when the controlling product standard, drawing, or approved project schedule requires them or when they close a defined acceptance risk. If engineering has not fixed values, provide the route and concern for review rather than inventing a generic range.
How should buyers avoid unclear hardness requirements?
Name the method, exact scale or force, target, material state, preparation, curvature/support basis where relevant, test locations, sample extent, lot definition, frequency, judgment and retest rule, and required actual report fields. Never write only a number or rely on an informal conversion.
RFQ checklist
- Drawing, project material schedule, customer specification, revision, and document-precedence hierarchy
- Grade, product/material standard, national adoption if applicable, and exact edition
- Product form, ordered dimensions, quantity, ruling section, thermal condition, and surface route
- Acceptance role for each value: design, product-standard, incoming process control, or informational
- Hardness method, exact scale/test force designation, target, preparation, support/curvature basis, and test state
- Hardness axial and radial locations, end distance, traverse sketch, spacing, number of readings, and frequency
- Individual versus average acceptance, rounding, measurement uncertainty treatment, retest, sorting, and rejection rule
- Tensile properties, units, test method, specimen geometry, orientation, and radial/axial location
- Section and material state represented by each specimen, heat and heat-treatment lot, frequency, and retest
- Lot definition by heat, diameter/section, condition, furnace batch or campaign, and no untraceable pooling
- Downstream machining, forging, heat treatment, straightening, grinding, coating, and final person accepting the result
- Inspection-document type, actual result fields, methods, specimen identity, linked reports, retests, and deviations
- Heat-to-bar/bundle traceability, marking, packing-list reconciliation, document-review timing, and release approval
- Third-party witness/hold points, notice period, waiver, nonconformance approver, and shipment release if required
- Separate supplier alternative matrix for method, scale, sampling or certificate deviations before manufacture
- Packing, preservation, bundle limits, destination, Incoterm, and requested shipment window
References
- ISO 6506-1:2014 Metallic materials — Brinell hardness test — Test method
- ISO 6507-1:2023 Metallic materials — Vickers hardness test — Test method
- ISO 6508-1:2023 Metallic materials — Rockwell hardness test — Test method
- ISO 6892-1:2019 Metallic materials — Tensile testing at room temperature
- ASTM A370-26 Standard Test Methods and Definitions for Mechanical Testing of Steel Products
- ISO 10474:2013 Steel and steel products — Inspection documents
- JOTAIN redacted 42CrMoA MTC example — technical fields only
- Low, S. R. III — NIST SP 960-5: Rockwell Hardness Measurement of Metallic Materials
Inquiry support
Need to tighten the inspection plan?
Send the drawing or RFQ with the grade, size, condition, processing, inspection, quantity, and destination. We can flag open points before quotation.